REACH Compliant Dog Carrier Backpack Materials
REACH compliance for a dog carrier backpack is managed per material, not per product. Any article containing a substance of very high concern above 0.1 percent by weight carries a communication duty, and Annex XVII restriction entries are absolute bans above defined limits. Six component classes carry the risk: coated textiles, dyed fabric, plastic trim, metal hardware, foam and prints. MOQ 500, samples 6-10 working days, bulk 35-50 days.
Executive Summary
REACH is a chemical regulation applied to articles, and the unit of compliance is the material rather than the finished carrier. A pet carrier is an assembly of eight to fifteen materials, each with its own chemical profile and each with its own obligation. The candidate list of substances of very high concern is updated periodically, the restriction list in Annex XVII applies absolute limits to defined substance and application combinations, and the 0.1 percent weight-by-weight threshold triggers a communication duty down the supply chain.
The practical programme is a restricted substance list in the tech pack, a conformance declaration per component, and targeted testing where a material class carries known risk. The framework is maintained by ECHA, and textile chemical conformance is commonly evidenced by per-material certification such as OEKO-TEX. Production terms are unaffected: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production 35-50 days, final inspection at AQL 2.5, FOB Xiamen under T/T 30/70.
Wholesale pet carrier programmes for dog carrier backpack ranges run 35-50 days after sample approval, shipped FOB Xiamen under T/T 30/70 terms.
Where REACH Applies in a Pet Carrier Build
REACH applies to substances, mixtures and articles placed on the European market, and a dog carrier backpack is an article. The obligations that attach to an article are narrower than those attaching to a chemical manufacturer, but they are real and they are enforceable at the point of import and at the point of sale.
Three obligations matter for a sewn carrier. The first is the restriction obligation: certain substances listed in Annex XVII may not be present above a defined limit in defined applications, and there is no de minimis argument. The second is the communication obligation: where a substance on the candidate list is present above 0.1 percent by weight in the article, information must be communicated down the supply chain and, for consumer articles, provided to a consumer on request within 45 days. The third is registration-related and generally falls on the importer or the EU-established representative rather than on the non-EU producer.
The unit of compliance is the material. Because a carrier is assembled from many materials, the correct approach is a component-level analysis rather than a finished-product test. Testing a finished carrier for the entire candidate list is expensive, slow and technically poor, because extraction from a bonded assembly is less reliable than extraction from a single material. Testing the coated shell, the dyed lining, the plastic trim and the metal hardware separately gives better data at lower cost.
One structural point decides whether the programme is manageable: the bill of materials must name the actual supplier and grade of every component. A BOM that says 600D polyester without naming the mill and the finish code cannot be assessed for chemical conformance, and no amount of finished-product testing compensates for that gap.
The importer's position deserves a specific note because it determines who is liable. Where a non-EU producer supplies a brand established in the European Union, the EU-established importer carries the obligation for articles it places on the market. The producer cannot discharge that obligation on the importer's behalf, but it can supply the evidence the importer needs. A buyer should therefore treat the technical file as its own asset and should require the documents rather than accept an assurance that they exist.
SVHC Candidate List, Annex XVII and the 0.1 Percent Threshold
Two lists with two different legal effects are routinely confused. Understanding the difference is most of the practical work.
The candidate list of substances of very high concern is a list of substances identified for possible inclusion in the authorisation list. Presence above 0.1 percent by weight in an article triggers a communication duty, not a ban. The list is updated periodically, which means a material that was unproblematic two years ago may carry an obligation today. The duty is met by providing sufficient information to allow safe use, and for consumer articles by responding to a consumer request within 45 days at no charge.
Annex XVII is the restriction list and it is different in kind. It lists substances with defined conditions of restriction, and where a substance and application combination is listed, the limit is absolute: the article may not be placed on the market if the limit is exceeded. Restrictions relevant to sewn goods include certain azo dyes that cleave to listed aromatic amines, certain phthalates in plasticised material, nickel release from articles in prolonged skin contact, and polycyclic aromatic hydrocarbons in certain rubber and plastic components.
The 0.1 percent threshold applies to the article as placed on the market, which for an assembled product means each component article within it. A zipper pull containing an SVHC above 0.1 percent by weight of that pull carries the duty even though it is a tiny fraction of the carrier's total mass. This is why component-level assessment matters: the threshold is calculated per article, not per finished assembly.
The practical response to the updating candidate list is a periodic review rather than a one-time test. A quarterly check of the list against the declared composition of each component is a few hours of work and is what prevents a material from silently becoming non-conformant.
The two lists also produce different commercial consequences, and the difference is worth stating because it shapes how a brand should respond to a finding. A candidate list hit creates a communication duty and a reputational question, but it does not of itself stop the product being sold. An Annex XVII breach stops the product at the border and requires withdrawal of what has already been placed on the market. The response to the first is documentation and substitution planning; the response to the second is urgent and expensive.
High-Risk Materials in a Sewn Carrier: A Component-by-Component Map
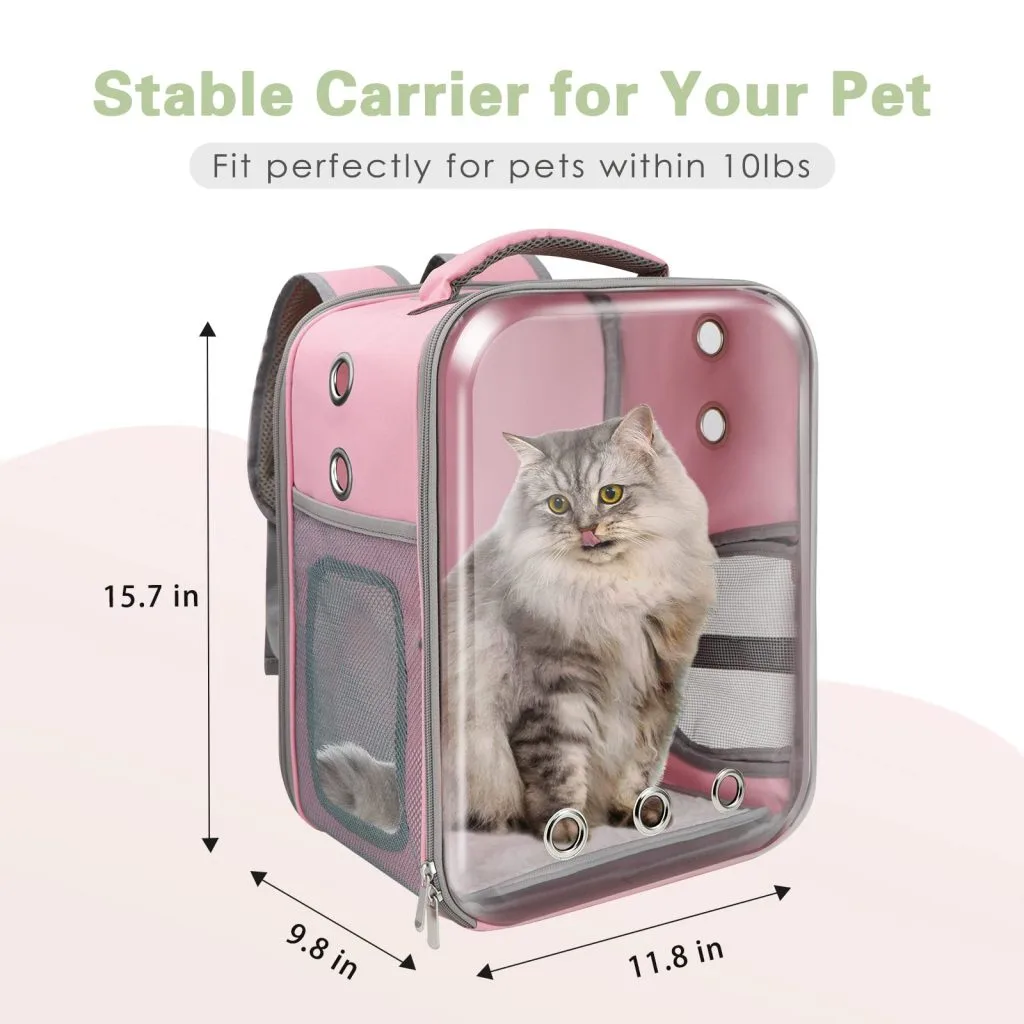
Not every component carries equal risk. Six classes account for almost all realistic findings in a pet carrier build, and mapping them is what makes a testing budget efficient.
| Component | Typical chemistry | Relevant concern | Control |
|---|---|---|---|
| PVC coated shell | Plasticiser system | Phthalate restriction entries | Declaration plus targeted test |
| PU coated shell | solvent or solvent-free PU | Residual solvent, SVHC in catalysts | Supplier declaration |
| Dyed fabric and lining | Disperse and reactive dyes | Azo dyes cleaving to listed amines | Per-shade test |
| Printed areas | Pigment or plastisol ink | Phthalates, heavy metal pigments | Ink declaration plus test |
| Metal hardware | Zinc alloy, steel, plating | Nickel release, lead and cadmium | Per-finish test |
| Foam and board | EPE, EVA, PU foam | Flame retardants, residual monomers | Supplier declaration |
| Webbing and tape | Polypropylene or polyester | Dyestuff, finishing agents | Covered by textile certificate |
| DWR finish | Fluorinated or paraffin finish | Perfluorinated compounds | Declaration, screening test |
PVC coated fabric is the single highest-risk component in a carrier build, because the plasticiser system that gives PVC its hand and flexibility is the chemistry most often restricted. A supplier declaration stating that the coating is phthalate-free is worth requesting specifically, and where a soft, flexible coated hand is required, a polyurethane coating is the lower-risk alternative with a modest cost premium.
Dyed textiles are the second area, and the relevant point is that risk is per shade rather than per fabric. A fabric mill may supply an identical base cloth in twelve colours with six different dye formulations, and a certificate covering the black version says nothing about the pale grey one. Pale and bright shades generally carry more risk than black, which is counterintuitive and frequently missed.
Metal hardware is the third and the most testable. Nickel release is a migration test rather than a content test, and it applies to components in prolonged contact with skin - buckles, sliders, D-rings and any metal that touches the hands during carrying. Plating quality varies by batch, so a per-finish test with annual re-verification is the standard control.
Foam and board are the fourth and are the class most often ignored, largely because they are hidden inside the product. Flame retardant additives are the historical concern in flexible polyurethane foam, and residual monomer content is the concern in expanded polymers. Neither is likely in a modern pet carrier supply chain, but neither can be excluded without a declaration, and a declaration is free. The practical rule is that no component is low-risk enough to skip the paperwork.
Testing Strategy: Material-Level Versus Article-Level
The choice between testing materials and testing finished articles determines both cost and data quality, and the answer is almost always materials.
Material-level testing submits each component separately: the coated fabric as a fabric swatch, the webbing as a length, the hardware as a bag of parts. Extraction is clean, the result is attributable to a named supplier, and a failure can be fixed by changing one component. Cost scales with the number of distinct materials, typically eight to twelve for a carrier, and a full panel across those materials is a defined and predictable expense.
Article-level testing submits the assembled carrier. It costs more per sample because the laboratory has to dissect and separate, it produces results that are hard to attribute to a specific component, and a failure means re-testing each candidate material anyway. Its one advantage is that it captures cross-contamination during assembly, which is rare in a sewn product and common in an adhesively bonded one.
The recommended strategy is a hybrid. Declarations cover every component. Targeted testing covers the six high-risk classes, per shade for dyed textiles and per finish for metal. Article-level screening is reserved for a first-season program or after a component substitution, as a verification that the assembly introduced nothing.
Sampling discipline matters more than test volume. Testing one material from one supplier once and applying the result to all suppliers of that material class is the common error. A result belongs to a named supplier, a named grade and a named shade, and it travels no further than that.
Budget is the practical constraint and it shapes the strategy. A targeted panel on the six high-risk classes across eight to twelve materials is a defined, manageable cost that a first-season programme can carry. Screening every material for the full candidate list is not, and it produces a large volume of results that nobody has time to interpret. The efficient allocation is declarations everywhere, tests on the risk map, and re-testing on change, which concentrates spend where the probability of a finding is real.
Documentation: Declarations, Safety Data Sheets and Evidence
Testing is verification; documentation is the programme. Three document types carry a REACH conformance case, and each has a specific role.
A supplier conformance declaration is the base layer. It is issued by the component supplier and states that the material conforms to the buyer's restricted substance list, naming the material, the grade, the shade and the date. Where the supplier is outside the EU the declaration is addressed to the buyer as the importer. Declarations are cheap, they scale across the whole bill of materials, and they are the only practical way to cover every component rather than only the risky ones.
Safety data sheets apply to preparations rather than articles, but they are the right document for inks, coatings, adhesives and finishing agents as supplied. An ink supplier's safety data sheet states the composition of the ink as delivered, and cross-checking it against the restricted substance list is a ten-minute exercise that catches most problems before they reach a laboratory.
Test reports are the verification layer, and they should be dated within two years, issued by an accredited laboratory, and name the method and the result against a stated criterion. A report on a material that is not the material being supplied is worthless, and the check is the supplier and grade code on the report against the code on the bill of materials.
Per-material certification schemes occupy a middle position and are widely used in textiles. A certificate such as those issued under the OEKO-TEX system covers a defined set of restricted substances for a named textile material, is renewed periodically, and is accepted by most European retailers as sufficient evidence for the covered parameters. It does not cover metal hardware or plastic trim, so a programme still needs declarations and targeted tests for those.
UK REACH, California and Other Parallel Regimes
REACH is not the only chemical regime a carrier programme has to satisfy, and the parallel regimes differ in structure rather than merely in name.
UK REACH operates separately following the United Kingdom's departure from the European Union, with its own candidate and restriction lists maintained by the UK authorities. For a transitional period the UK list substantially mirrored the EU one, but the two now diverge as each is updated independently. A brand selling into both markets should assess against both lists, and should not assume that an EU declaration covers Great Britain.
California's Proposition 65, administered through OEHHA, is structurally different: it is a warning obligation rather than a restriction. Where a listed substance is present above a safe harbour level, a clear and reasonable warning must be given before exposure. The determination is made by testing rather than by declaration, and the outcome is frequently that no warning is required. The overlap with REACH is partial, because the listed substances differ.
US federal requirements, administered by the US Consumer Product Safety Commission, centre on lead content and specified phthalates in accessible components, and, where a product is sold in a children's channel, on a certificate supported by third-party testing. The concept of accessible component is different from the REACH concept of article, and a programme should not assume one test covers both.
Other jurisdictions add specifics: several US states are restricting perfluorinated compounds in textiles independently of federal action, and Japan and Canada apply their own textile chemical requirements. The efficient response is a single master restricted substance list that unions all of the applicable regimes, with a declaration required against that one list rather than against each market separately.
Maintaining Conformance Across Seasons and Suppliers
A conformance case that is built once and never revisited will fail, because the candidate list changes, suppliers change, and specifications drift. Four controls keep it current.
Periodic list review is the first. The candidate list is updated regularly, and each update should trigger a check of the declared composition of every component against the new entries. This is a desk exercise against supplier declarations, and it is the only way to catch a material that became non-conformant without changing.
Change control is the second. Any substitution of a component, a mill, a finish or a dye formulation should require a new declaration and, for a high-risk class, a new test. The most common route to non-conformance is a substitution made for cost reasons and not notified, which is why the change-control clause in the supply agreement matters more than any test.
Annual re-testing is the third. Declarations persist; test results age. A reasonable cadence is annual re-testing of the high-risk classes - coated fabric per shade, printed areas, metal per finish - with full re-testing on any change.
Supplier re-qualification is the fourth. A component supplier should be re-qualified on a defined cycle, and immediately after any declaration that cannot be substantiated. A supplier that will not provide a declaration naming the specific grade is communicating something, and the correct response is to qualify an alternative rather than to accept a general assurance.
The record that results - a bill of materials with named suppliers, a declaration per component, test reports per risk class, and a dated review log - is the technical file. It is what a market surveillance authority asks for, and it is what converts a chemical compliance claim from an assertion into evidence.
One final control is worth adding because it is the only one that tests the programme rather than the paperwork: a periodic blind re-test. Once a year, take a component from a current shipment and submit it to the laboratory without telling anyone which declaration it belongs to. The result either matches the file or it does not, and a mismatch reveals a substitution, a stale declaration or a supplier that has quietly changed formulation. It is the cheapest available check on whether the system is actually working.
What a Buyer Should Require in the Tech Pack
Everything in this article resolves to a small number of lines in the tech pack. Written correctly at the outset, chemical compliance costs paperwork rather than rework.
The tech pack should contain a restricted substance list, versioned and dated, that unions the applicable regimes. It should contain a bill of materials that names the supplier and grade of every component rather than describing it generically. It should state the required evidence per component: declaration, test report, or both. It should require declarations before sampling rather than before shipment, so that a problem surfaces while the specification can still change.
It should also state what happens on a failure. A material that fails a restriction test is not a candidate for a tolerance negotiation; it is replaced. Stating that in the tech pack removes the argument at the point where it is most expensive.
Two further lines are worth including because they cost nothing and prevent recurring problems. The first requires the supplier to notify any change of component source or formulation in writing before shipment. The second requires a per-shade declaration for dyed textiles, which is the single most commonly missed item in a textile compliance file.
The commercial framing is simple. Chemical compliance is procured, not tested in. A programme that specifies its materials, requires declarations at sampling and re-verifies annually spends a defined amount on paperwork; a programme that tests a finished product at the end and hopes spends unpredictably on rework, and occasionally on a withdrawn shipment.
The final line of the tech pack is the one that costs the least and saves the most: a named contact on both sides responsible for the chemical file. Most compliance failures are not technical failures, they are coordination failures in which a declaration was requested from nobody in particular and therefore arrived from nobody at all. One named owner per side converts the whole programme from an aspiration into a task with a deadline.
Why brands source here
- Pet carrier programs run since 2014; founding team in sewn goods since 2004
- SGS-verified production floor of 4,950 m² with 137 workers across 7 lines
- Monthly capacity of 200,000 units, audited to BSCI and ISO 9001
People Also Ask
What is REACH compliance for pet products?
Conformance to the EU chemical regulation assessed per material: no Annex XVII restriction exceeded, and a communication duty where a candidate list substance exceeds 0.1 percent by weight in a component.
How do you make a pet carrier REACH compliant?
Specify a restricted substance list in the tech pack, name the supplier and grade of every component, require a declaration per component before sampling, and test the six high-risk classes targeted by shade and finish.
Which materials in a carrier are highest risk?
PVC coated fabric for plasticisers, dyed textiles for azo dyes, printed areas for phthalates and pigments, metal hardware for nickel release, foam for flame retardants, and durable water repellent finishes for fluorinated compounds.
Is a finished product test enough for REACH?
No. It costs more, attributes poorly and cannot fix a failure without re-testing each component. Article-level screening is useful only as verification after a substitution.
How often does the SVHC candidate list change?
It is updated periodically, which is why conformance requires a quarterly desk review of declared compositions against new entries rather than a one-time test.
Do US and EU chemical rules overlap?
Partly. US federal requirements centre on lead and specified phthalates in accessible components, California adds a warning obligation, and the concept of accessible component differs from the REACH concept of article.
Frequently Asked Questions
Is REACH compliance tested on the finished carrier or per material?
Per material. Extraction from a single material is more reliable than from a bonded assembly, a result can be attributed to a named supplier, and a failure can be fixed by replacing one component.
What does the 0.1 percent threshold apply to?
To each article as placed on the market, which for an assembled carrier means each component article within it. A zipper pull above 0.1 percent carries the duty even though it is a tiny fraction of total mass.
What is the difference between the candidate list and Annex XVII?
The candidate list triggers a communication duty above 0.1 percent and is updated periodically. Annex XVII restrictions are absolute limits for defined substance and application combinations, with no de minimis argument.
Which component carries the highest risk in a carrier build?
PVC coated fabric, because the plasticiser system that provides flexibility is the chemistry most often restricted. A polyurethane coating is the lower-risk alternative with a modest cost premium.
Does a certificate for black fabric cover the same fabric in another shade?
No. Risk is per shade because dye formulations differ. Pale and bright shades generally carry more risk than black, which is counterintuitive and frequently missed.
How often should chemical testing be repeated?
Annually for the high-risk classes - coated fabric per shade, printed areas, metal per finish - with full re-testing on any change of component, mill, finish or dye formulation.
Is UK REACH the same as EU REACH?
They are separate regimes with separate candidate and restriction lists that are now updated independently. An EU declaration does not automatically cover Great Britain.
Does an OEKO-TEX certificate cover metal hardware?
No. It covers textile materials for a defined set of restricted substances. Metal hardware and plastic trim still require declarations and targeted testing for nickel release and restricted plasticisers.
What should a supplier declaration state?
Conformance to the buyer's restricted substance list, naming the material, the grade, the shade and the date. A general assurance without those specifics does not support a compliance case.
How long are test reports valid?
Treat reports older than two years as indicative rather than current, because both the method and the material supply chain may have changed. Declarations also need periodic renewal.
What happens if a material fails a restriction test?
It is replaced. A restriction limit is not a tolerance to be negotiated, and stating that in the tech pack removes the argument at its most expensive point.
Should declarations be required before sampling?
Yes. Requiring them at sampling surfaces a problem while the specification can still change; requiring them before shipment is too late to do anything but rework.
Talk to QUANZHOU JUNYUAN BAGS about a pet carrier program: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample