Cat Carrier Pet Vlogger: Video Production
A video-ready cat carrier needs shape retention within 4 mm under pan, exterior gloss held at 3-8 GU to survive a key light, material rustle below 35 dB(A) at 1 m, and a mesh aperture of 2.0-2.8 mm to avoid sensor moire. Sampling runs four rounds, the third of which is shot in a mock studio before bulk is released.
Video is a harsher medium than stills for a sewn product, because it adds time and sound to the specification. A still has to look right in one frame; a video has to look right in every frame while the product moves, while the light moves, and while a microphone sits one metre away. This page sets out the four variables that decide whether a cat carrier performs on video: shape retention through a pan, spectral behaviour under continuous light, gloss and specular control, and acoustic signature. Each is a manufacturing variable with a number attached, and each costs money to specify, so the page also gives the cost model and the sampling cadence. Commercial terms follow the standard programme: MOQ 500 pieces per colourway, prototypes in 6-10 working days, bulk production 35-50 days after sample approval, final random inspection to AQL 2.5, T/T 30/70 and FOB Xiamen. What a video programme changes is the number of sample rounds, because the third round is judged on footage rather than on a physical inspection.
Audit records from a dog carrier factory remain the fastest way to separate a real cat carrier production base from a trading office with a photo catalogue.
Frame-Level Requirements: Shape Retention and Pan Behaviour
A video moves the camera around the product, and a soft product deforms while the camera moves. The deformation is not visible in a single frame but it is obvious across a pan, where a bag that starts square and ends slumped reads as a different object from the one in the opening shot.
The measurable target is shape retention: with the product loaded to 4 kg and suspended from its handle, the deviation of any external edge from its unloaded position must be under 4 mm after 60 seconds and under 8 mm after 10 minutes. Meeting that requires structure rather than more fabric, and the structure has to be specified.
The elements that deliver it are a base board, side stiffeners and a tensioned panel. A base board of 3-5 mm EVA or a moulded polypropylene sheet at 350-600 g/m2 equivalent stops floor sag, which is the largest single contributor. Side stiffeners of 1.5-3 mm at 60-120 mm width stop the panel collapsing inward between the top and bottom seams. A tensioned shell — cut slightly undersized against the frame — keeps the fabric drum-tight rather than slack.
| Element | Specification | Sag at 60 s (mm) | Sag at 10 min (mm) | Added cost (USD) | Weight added (g) |
|---|---|---|---|---|---|
| No structure | Fabric shell only | 14-22 | 25-40 | 0 | 0 |
| Base board only | 3 mm EVA | 7-12 | 13-20 | 0.35-0.90 | 60-110 |
| Base board plus side stiffeners | 3 mm plus 2 mm rails | 3-5 | 6-9 | 0.85-1.90 | 140-240 |
| Full frame plus tensioned shell | 4 mm board, rails, undersized cut | 1-3 | 2-5 | 1.40-2.80 | 210-360 |
| Moulded shell insert | Injection-moulded frame | Under 1 | 1-2 | 3.20-6.50 | 320-540 |
Weight is the trade against structure, and video makes it sharper than usual. Every 100 g added is 100 g on a gimbal, and a handheld stabiliser with a 1.2 kg payload rating has little margin once a carrier and an animal are on it. The working compromise for a video-facing SKU is the third row of the table: base board plus side stiffeners at 140-240 g, which holds sag under 5 mm while keeping the unit at 1.1-1.5 kg.
The second deformation to specify is handle stretch. A webbing handle elongates 2-6% under a 4 kg load, which across a 200 mm handle is 4-12 mm of visible droop mid-shot. Specifying a low-stretch webbing with an elongation under 2% at 400 N removes it for 0.15-0.40 USD.
Shape retention on video is a base board, side rails and a low-stretch handle, and the target is under 4 mm of edge deviation after 60 seconds under load.
Colour Under Continuous Light: CRI, TLCI and Spectral Reflectance
Continuous light is not daylight, and a fabric matched under D65 can shift badly under an LED panel with a poor spectral profile. The shift is worst in exactly the colours most used in this category: deep navy, warm beige and mid-grey.
The two indices that matter are CRI and TLCI. A panel at CRI 95 or above and TLCI 90 or above reproduces a dyed fabric close to its daylight appearance. Below CRI 85, saturated blues and warm neutrals shift by Delta-E 3-6, which is visible without a reference and obvious with one. A manufacturer cannot control the creator's lighting, but can control how sensitive the fabric is to it.
Sensitivity is reduced by choosing dyes with a broad, smooth reflectance curve rather than a spiky one. Spiky reflectors — some bright blues, some fluorescent-adjacent greens — change appearance with the light source; broad reflectors do not. The practical instruction to the dye house is a reflectance curve with no single-band spike above 15% of the mean across 400-700 nm.
| Colourway | Shift at CRI 95, Delta-E | Shift at CRI 85, Delta-E | Shift at CRI 75, Delta-E | Recommendation |
|---|---|---|---|---|
| Mid grey | 0.8-1.4 | 2.2-3.4 | 4.0-6.2 | Avoid for video-led SKUs |
| Warm beige | 1.0-1.8 | 2.6-4.0 | 4.8-7.0 | Specify broad-reflectance dye |
| Deep navy | 1.4-2.4 | 3.4-5.2 | 6.0-9.0 | Avoid, collapses to black |
| Sage green | 0.8-1.5 | 2.0-3.2 | 3.8-5.6 | Good video performer |
| Terracotta | 0.6-1.2 | 1.6-2.6 | 3.0-4.6 | Best video performer |
| Charcoal | 1.0-1.6 | 2.4-3.6 | 4.2-6.4 | Acceptable with matte finish |
Exposure headroom is the second colour issue and it is about the tonal range a sensor can hold. A camera set for a mid-grey subject holds roughly 8-10 stops; a pure white fabric blows out and a near-black fabric crushes, and neither can be recovered. For a video-led colourway the useful reflectance range is 25-70%, which rules out optical white and rules out deepest black on the largest panels.
The material declaration still applies to everything that goes on camera, since the product is shot in extended contact with an animal. Declarations in this category are issued against OEKO-TEX criteria, and welfare guidance for filming animals is commonly cross-checked against material published by the American Veterinary Medical Association.
Specify broad-reflectance dyes and a 25-70% reflectance range; navy and grey are the two colourways most likely to fail under a poor LED panel.
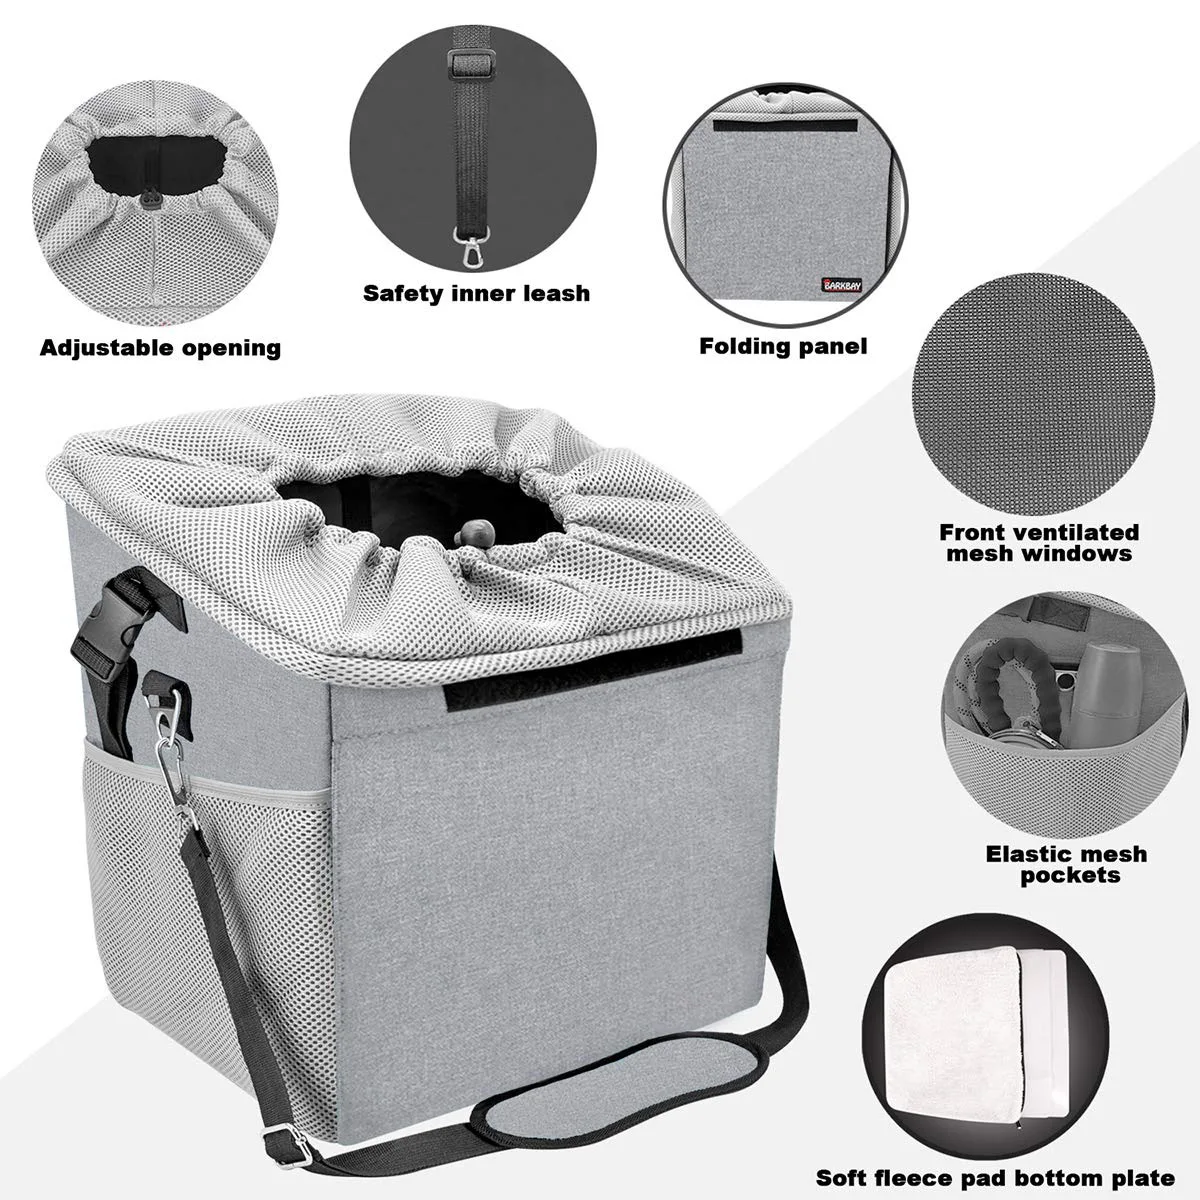
Specular Control: Gloss, Hotspots and Matte Trim Under a Key Light
A key light at 1.5-2.5 m produces a specular reflection on any surface glossier than about 15 GU, and that reflection is the most common visual defect in product video shot with limited lighting. It appears as a moving white patch that tracks the camera and that cannot be graded out.
The target for a video-facing exterior is 3-8 GU at 60 degrees with a maximum point reading of 12 GU. Achieving it requires a matting agent in the topcoat rather than a mechanical emboss, because an embossed surface polishes at wear points — handles, corners, strap contact — and a polished patch is worse than a uniformly semi-gloss surface, since it moves and changes size as the product turns.
Trim is glossier than fabric and needs its own call. A polished zipper pull at 80-120 GU is a small but high-contrast hotspot; a nickel-plated D-ring is larger. The specification for video is brushed or anodised metal at 20-40 GU, matte acetal for buckles and adjusters, and painted or anodised pulls. Across a full trim set the change costs 0.15-0.45 USD.
| Surface | Gloss target, 60 degrees | Failure mode on video | Specification | Added cost (USD) |
|---|---|---|---|---|
| Exterior shell | 3-8 GU, max 12 | Moving hotspot | Matting agent in topcoat | 0.20-0.60 |
| Top and side panels | 3-8 GU | Blown highlight | Same topcoat, verified per lot | Included |
| Zipper pull | 20-40 GU | Small high-contrast hotspot | Anodised or painted | 0.05-0.20 |
| Buckles and adjusters | Under 20 GU | Large hotspot | Matte acetal | 0.08-0.25 |
| D-rings and hardware | 20-40 GU | Hotspot plus movement glint | Brushed or anodised | 0.04-0.15 |
| Interior lining | 3-8 GU, mid tone | Low-contrast frame through mesh | Matte mid-tone, not black | 0.10-0.35 |
Verification has to happen on production fabric under a key light rather than on a swatch card, because a swatch held flat in the hand hides the curvature that creates the hotspot. The release test is a photograph of an assembled unit under a single 5600 K source at 2.0 m and 45 degrees, examined for any pixel above 240 on an 8-bit scale outside the intended highlight.
The interior lining deserves the last note. Video of the interior is shot through the mesh or through an open top, and a glossy black lining produces a frame in which a dark animal is invisible. A matte mid-tone lining at 3-8 GU gives a workable exposure range and is one of the cheapest improvements in the whole specification.
Gloss control is six surface calls verified under a real key light, and the interior lining is the cheapest of them.
Audio Signature: Material Rustle and Hardware Noise in dB(A)
Audio is the variable manufacturers omit most often, and it is the one that most reliably ruins otherwise good footage. A microphone at 0.8-1.5 m picks up every rustle, tap and rattle from the product, and post-production noise reduction on product rustle produces artefacts that are often worse than the original.
The measurable target is material rustle below 35 dB(A) at 1 m under a standardised handling cycle: pick up, rotate 90 degrees, set down, open and close one zipper. A coated polyester shell with a stiff hand typically measures 42-55 dB(A); a soft-hand nylon or a brushed face measures 30-38 dB(A).
Hand stiffness is the controlling property, and it is set by coating weight and by any laminated layer. A coating of 30-40 g/m2 gives a soft hand; 60-80 g/m2 gives a stiff, noisy one. The conflict with durability is real: heavier coatings abrade better. The resolution used in production is a lighter topcoat plus a separate abrasion-resistant finish, which holds both properties at 0.25-0.70 USD.
| Component | Measured level, dB(A) at 1 m | Character | Mitigation | Reduction (dB) | Cost (USD) |
|---|---|---|---|---|---|
| Stiff coated shell, 60-80 g/m2 | 42-55 | Broadband rustle | Lighter topcoat, soft-hand finish | 8-14 | 0.25-0.70 |
| Metal zipper chain | 38-48 | 2-6 kHz rattle | Coil chain, moulded pull | 6-12 | 0.20-0.55 |
| Free D-ring against shell | 34-44 | Impact tap | Bonded trim tail or sleeve | 10-18 | 0.05-0.15 |
| Strap adjuster | 30-40 | Impact tap | Silicone sleeve | 8-15 | 0.06-0.18 |
| Hook-and-loop closure | 52-68 | Tear, very broadband | Replace with magnetic or cam closure | 20-30 | 0.40-1.20 |
Hook-and-loop is the single loudest closure in the category and it deserves specific attention. At 52-68 dB(A) it is louder than the product's entire remaining signature and it occupies the frequency range where voice sits. Where a video programme needs a quiet closure, a magnetic closure or a cam buckle replaces it at 0.40-1.20 USD, with the caveat that magnetic closures need a pull-force specification of 25-45 N to remain escape-resistant.
Measurement protocol matters for the numbers to be comparable: a calibrated sound level meter at 1 m, A-weighting, in a room with a background under 30 dB(A), with the handling cycle performed at a standardised 0.5 m per second. Without the protocol the figures are not reproducible and a supplier claim of quiet cannot be checked.
Audio is a specification with a number: under 35 dB(A) at 1 m, achieved through coating weight, a coil zipper and the elimination of hook-and-loop where voice is being recorded.
Mesh, Moire and Rolling Shutter: Structural Patterns on Sensor
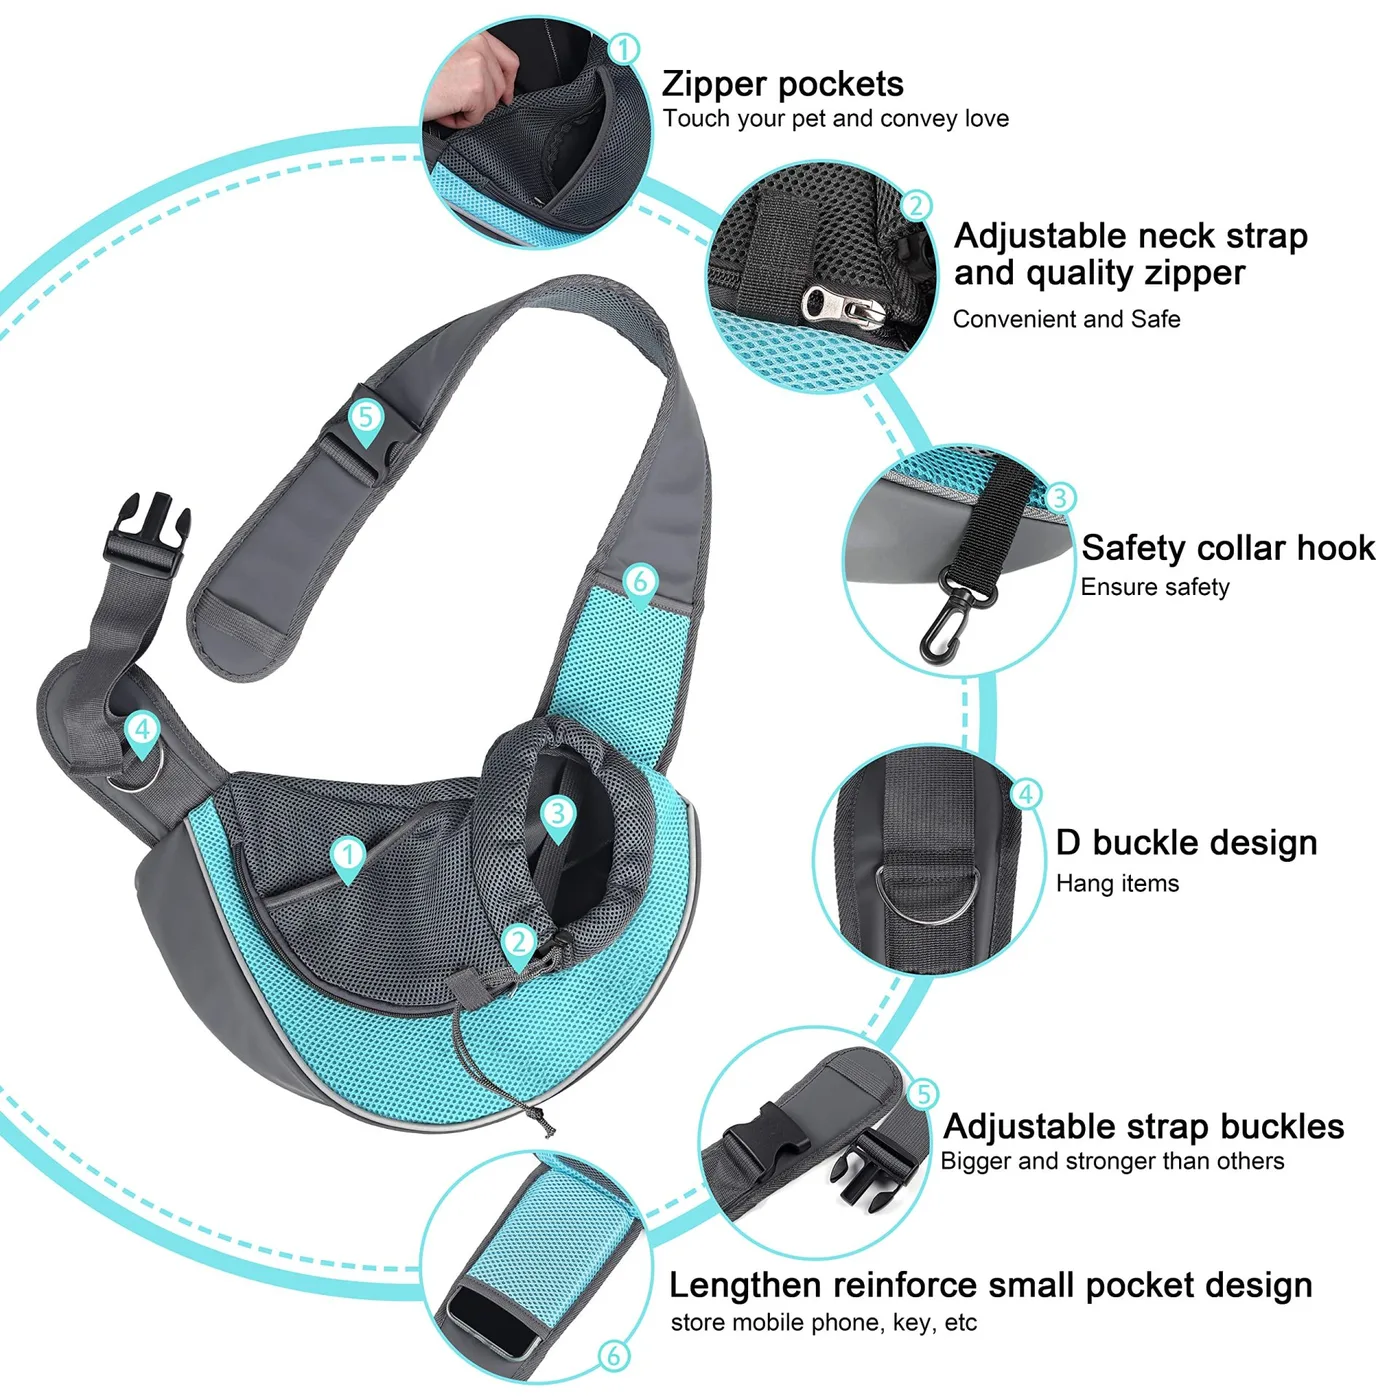
A regular woven structure interacting with a sensor sampling grid produces moire, and a moving camera with a rolling shutter produces skew. Both are structural properties of the product interacting with the capture device, and both have manufacturing answers.
Moire risk rises as the aperture approaches the sensor's sampling interval. A mesh at 1.0-1.5 mm aperture is the worst case for a phone or a consumer camera at typical product distances; moving to 2.0-2.8 mm removes the interference in most configurations. Where ventilation is a claimed property, the number to hold is open area, not aperture: a 2.4 mm aperture at 40% open area moves the same air as a 1.2 mm aperture at 40%.
Rolling shutter skew appears on any strong vertical or horizontal edge when the camera pans quickly, and it is worst on high-contrast straight lines. A product with long uninterrupted seams and straight webbing runs shows skew visibly; one with broken lines, curved edges and a textured surface hides it. That is a design instruction rather than a tolerance, and it is cheaper to apply at pattern stage than to fix later.
| Aperture (mm) | Filament | Open area (%) | Moire risk | Airflow index | Recommended |
|---|---|---|---|---|---|
| 0.8-1.2 | Monofilament | 30-38 | Severe | 100 | No |
| 1.2-1.8 | Monofilament | 35-45 | High | 112 | No for video |
| 2.0-2.8 | Texturised | 35-45 | Low | 118 | Yes |
| 2.8-3.6 | Texturised | 40-52 | Very low | 128 | Yes, where claw resistance allows |
| Hexagonal, 3-5 mm | Texturised | 45-58 | Very low | 135 | Yes, best airflow |
Claw resistance sets the upper bound on aperture. A monofilament above roughly 2.5 mm aperture is more easily caught and pulled by a claw, so the upper rows of the table need a filament specification with a tensile strength above 300 N and a snag test. The hexagonal structure at 3-5 mm performs best on both axes but requires a coated or welded junction to resist snagging.
Flicker is the third sensor artefact and it is a lighting issue with a material consequence. An LED panel with pulse-width dimming below about 1,500 Hz produces banding on a product with a smooth, uniform surface, because the uniform surface makes the banding easy to see. A textured shell face breaks it up; a smooth glossy face does not.
Mesh specification for video is aperture 2.0-2.8 mm at 35-45% open area, on a texturised filament, with a snag test setting the upper bound.
Rigging, Mounting and Payload: Weight and Attachment Geometry
Video production mounts product. It goes on a tripod, on a gimbal, on a slider, on a turntable or on an overhead rig, and each imposes a payload and an attachment requirement that a retail product does not have to meet.
Payload is the first constraint and it interacts with the structure decisions from the first section. A consumer gimbal rated at 1.2-1.6 kg has to carry the carrier plus an animal, so a 1.4 kg structured unit plus a 4.5 kg cat is far outside it and the shot will not stabilise. Where a creator uses a gimbal, the specification target is a bare unit weight under 1.2 kg, which pushes the structure toward the lighter rows of the table and accepts 6-9 mm of sag.
Attachment geometry is the second. An overhead rig needs a rigid, symmetric point; a turntable needs a flat, non-slip base; a slider needs a low centre of gravity. The manufacturing answers are a reinforced overhead lift point rated to three times unit weight, a flat base with a coefficient of friction above 0.4, and a low-slung internal ballast pocket that lets the operator drop the centre of gravity by 40-80 mm.
| Provision | Serves | Specification | Added cost (USD) | Weight added (g) | Visible in frame |
|---|---|---|---|---|---|
| Reinforced overhead lift point | Overhead rig, crane | Rated 3x unit weight, 400 N min | 0.45-1.10 | 25-60 | Yes, removable cap |
| Flat non-slip base | Turntable, tabletop | Coefficient of friction above 0.4 | 0.25-0.60 | 30-70 | No |
| Internal ballast pocket | Slider, gimbal balance | Accepts 200-500 g, centred | 0.30-0.75 | 20-40 | No |
| Quarter-inch threaded insert | Tripod plate | Brass insert in base board | 0.55-1.30 | 15-35 | No, under base |
| Removable strap set | Clean frames without straps | Quick-release, 300 N | 0.70-1.60 | 60-120 | Yes when fitted |
A quarter-inch threaded insert in the base board is the single most useful provision for a video programme and it is often omitted because it is invisible in normal use. At 0.55-1.30 USD it converts the product from something that has to be propped to something that mounts, and it removes the improvised clamps that damage the shell.
Removable straps are the second most useful, because straps are the element most likely to spoil a composition. A quick-release strap set rated to 300 N lets a creator shoot a strapless product for the beauty frames and refit for the carry frames, and it is the difference between one product and two looks.
Mounting provisions cost 1.50-4.00 USD in total and turn an object that has to be propped into one that can be rigged.
Sampling Cadence for a Video Programme: Four Rounds
A video programme needs one more sample round than a wholesale programme, because between the colour round and the bulk release there has to be a round that is judged on footage. Physical inspection cannot detect moire, rustle or hotspot, and those are the failures that matter here.
Round one is the construction sample at 6-10 working days, judged on geometry and structure, with the shape-retention measurement performed under a 4 kg load. Round two is the colourway sample at 6-10 working days, judged under 5600 K continuous light and measured for gloss at six points. Round three is the camera test sample at 5-8 working days — two to three units built on the production line from bulk materials and shipped for a studio test. Round four is the pre-production confirmation at 5-8 working days, incorporating whatever the footage found.
The camera test round is the one to protect. It requires a defined shot list rather than a free-form test: a 360-degree pan, a static 10-second hold under a single key light, a zipper open and close at 1 m from a microphone, an interior shot through the mesh, and a pick-up and set-down cycle. The shot list makes the round repeatable and gives the production team specific measurements to change.
| Round | Duration | Units | Judged on | Measurements taken | Cost (USD) |
|---|---|---|---|---|---|
| 1 Construction | 6-10 working days | 1 | Physical inspection | Sag at 60 s and 10 min, handle stretch | 45-120 |
| 2 Colourway | 6-10 working days | 1 per colourway | Studio light | Delta-E at D65 and 5600 K, gloss 6 points | 30-70 each |
| 3 Camera test | 5-8 working days | 2-3 | Footage, defined shot list | Moire, hotspot above 240, rustle dB(A) | 50-90 each |
| 4 Pre-production | 5-8 working days | 2 | Footage plus inspection | Full re-test of round 3 metrics | 40-80 each |
| Bulk production | 35-50 days | Full order | AQL 2.5 | Lot colour and gloss release | Unit cost |
The calendar total is 22-36 working days of sampling plus 8-15 days of courier transit across four rounds, so 6-10 weeks from brief to bulk release. Compressing it is possible by merging rounds two and three, which saves 5-8 days and costs the ability to correct colour before the camera test — a reasonable trade for a repeat programme on an established pattern and a poor one for a new one.
Sample cost across the four rounds is 165-430 USD for a single colourway and 300-780 USD for three, credited against bulk orders above 1,500 units. Method references for the measurements follow published practice at ASTM International, which is what makes the numbers in the shot list checkable by the creator.
Four rounds, 6-10 weeks, and the third is judged on footage against a defined shot list rather than on a physical inspection.
Production Scheduling for Video Drops and Restocks
Video content has a longer shelf life than a social post and a shorter one than an evergreen review, which puts a video-led SKU in an awkward scheduling position: demand arrives in a spike, decays over 4-12 weeks, and may or may not recur.
The scheduling answer is a two-batch plan. The first batch is sized to the expected spike plus 20-30%, produced on the standard 35-50 day cycle and shipped by sea at 0.75-2.40 USD per unit. The second batch is a contingency, produced only if the spike exceeds forecast, and it is the one that uses air.
Sizing the first batch is the hard part and it is worth being explicit about the inputs. A creator with 200,000 subscribers converting at 0.3-1.2% on a 59 USD product generates 600-2,400 units of first-week demand; a creator with 800,000 subscribers converting at the same rate generates 2,400-9,600. Ordering to the midpoint of that range and holding air contingency is usually cheaper than ordering to the top and holding stock.
| Scenario | Batch 1 by sea | Batch 2 by air | Freight cost (USD) | Stockout risk | Blended freight per unit |
|---|---|---|---|---|---|
| Order to midpoint, no spike | 1,500 units | None | 1,125-3,600 | Moderate, 25-40% | 0.75-2.40 |
| Order to midpoint, spike | 1,500 units | 400 units air | 4,325-8,400 | Low | 2.28-4.42 |
| Order to top of range | 2,600 units | None | 1,950-6,240 | Very low | 0.75-2.40 |
| Order to top, no spike | 2,600 units | None | 1,950-6,240 | None, 1,100 excess | 0.75-2.40 plus holding |
| Order low, reorder by sea | 900 units | 900 units sea | 1,350-4,320 | High, 61-84 day gap | 0.75-2.40 |
Holding cost is what makes the top-of-range order expensive even when it sells. Excess stock of 1,100 units at 17 USD carried for 12 months costs 2,200-3,700 USD in capital and warehousing, which is comparable to the air freight it was meant to avoid. The rule that follows is to order to the midpoint and hold air contingency whenever the forecast range is wider than about 2.5 times.
Reorder timing is the second decision. A reorder at 500 units takes 35-50 days to produce; by sea it lands 61-84 days after the order, by air 41-59 days. Against a demand spike that decays over 4-12 weeks, only the air option arrives inside the demand window, which is why air is the default for a video restock and sea is the default for the initial build.
Order the spike to the midpoint by sea, hold air contingency, and accept that a video restock has to fly or it arrives after the demand has gone.
Cost Model: Video-Ready Specification and Replenishment Economics
Video readiness is bought with six specification changes and one extra sample round. The changes are individually cheap and collectively material, and the arithmetic is worth seeing in full before deciding which to take.
The six changes, against a 15.40 USD baseline unit at 500 pieces per colourway: structural package at 0.85-1.90 USD, soft-hand low-noise finish at 0.25-0.70 USD, matte hardware at 0.15-0.45 USD, quiet coil zipper at 0.20-0.55 USD, texturised mesh at 0.10-0.40 USD, and mounting provisions at 1.50-4.00 USD. Total 3.05-8.00 USD, which is a 20-52% uplift on the baseline.
That is a large uplift and it should be taken selectively. A creator shooting a static product review on a tripod needs structure, matte finish and the quiet zipper, and does not need mounting provisions or a gimbal-legal weight. A creator shooting moving b-roll needs all six. Segmenting the specification by shooting style is where the money is saved.
| Element | Baseline | Tripod review | Handheld b-roll | Full rig package |
|---|---|---|---|---|
| Base unit cost | 15.40 | 15.40 | 15.40 | 15.40 |
| Structural package | 0 | 1.20 | 1.20 | 2.10 |
| Soft-hand low-noise finish | 0 | 0.45 | 0.45 | 0.70 |
| Matte hardware | 0 | 0.28 | 0.28 | 0.45 |
| Quiet coil zipper | 0 | 0.35 | 0.35 | 0.55 |
| Texturised mesh 2.0-2.8 mm | 0 | 0.00 | 0.25 | 0.40 |
| Mounting provisions | 0 | 0.55 | 0.55 | 2.60 |
| Total per unit | 15.40 | 18.23 | 18.48 | 22.20 |
| Uplift over baseline | 0% | 18% | 20% | 44% |
Replenishment economics complete the model. At a landed cost of 22.50-27.00 USD for a tripod-review specification and a 59-79 USD retail price, gross margin is 55-70% before marketing. Air freight on a 400-unit contingency at 8-12 USD per unit consumes 20-30% of that margin on the air-shipped units, which is affordable on 400 units and not on 1,500.
The programme runs through the standard commercial frame, with the additions noted: MOQ 500 pieces per colourway, prototypes in 6-10 working days, bulk production 35-50 days after sample approval, final random inspection to AQL 2.5, T/T 30/70 and FOB Xiamen. Our production team builds video-led programmes through the SGS-verified production base under ISO 9001 and BSCI coverage. Video readiness costs 18-44% over a baseline unit, and the money is spent correctly only when the package matches the shooting style.
Order and quality terms
- MOQ 500 pieces per colourway; samples in 6-10 working days
- Bulk production 35-50 days after approval; AQL 2.5 inspection standard
- T/T 30/70 terms, FOB Xiamen, full document set per shipment
People Also Ask
What shape retention does a cat carrier need for video pans?
Under 4 mm of edge deviation after 60 seconds and under 8 mm after 10 minutes, with a 4 kg load suspended from the handle. That needs a base board plus side stiffeners at 140-240 g.
What gloss level avoids hotspots under a key light?
3-8 gloss units at 60 degrees with a maximum point reading of 12 GU, using a matting agent in the topcoat rather than a mechanical emboss, which polishes at wear points.
How loud is a typical cat carrier on a microphone?
42-55 dB(A) at 1 m for a stiff coated shell in a standard handling cycle. The target for video work is under 35 dB(A), reached with a lighter topcoat and a soft-hand finish.
Why is hook-and-loop avoided on video-facing products?
At 52-68 dB(A) it is louder than the rest of the product combined and it occupies the voice frequency range. A magnetic closure at 25-45 N pull force or a cam buckle replaces it.
What mesh aperture prevents moire on camera?
2.0-2.8 mm on a texturised filament at 35-45% open area. A 1.0-1.5 mm monofilament is the worst case, and open area rather than aperture is the number that governs airflow.
Which colourways perform worst under LED video lighting?
Deep navy shifts Delta-E 6.0-9.0 at CRI 75 and collapses to black; mid grey shifts 4.0-6.2 and reads as a different colour. Terracotta and sage are the most stable.
How many sample rounds does a video programme need?
Four: construction, colourway, a camera test round judged on a defined shot list, and a pre-production confirmation. Total 6-10 weeks from brief to bulk release.
Should a video restock ship by air or by sea?
By air. A reorder takes 35-50 days to produce and demand decays over 4-12 weeks, so sea at 61-84 days lands after the spike has passed and air at 41-59 days does not.
Frequently Asked Questions
Why is structure more important for video than for retail?
A camera pans around the product, and a soft product deforms while it moves. The deformation is invisible in one frame and obvious across a shot, where a bag that starts square and ends slumped reads as a different object.
How much weight does structural reinforcement add?
140-240 g for base board plus side stiffeners, or 210-360 g for a full frame with a tensioned shell. On a gimbal rated at 1.2-1.6 kg every 100 g matters.
How much does a webbing handle stretch under load?
2-6% under a 4 kg load, which is 4-12 mm of visible droop on a 200 mm handle. A low-stretch webbing with elongation under 2% at 400 N removes it for 0.15-0.40 USD.
What reflectance range should a video-facing colourway use?
25-70%. A sensor holds roughly 8-10 stops, so optical white blows out and near-black crushes, and neither is recoverable in grading.
Why should an embossed matte finish be avoided?
It polishes at wear points — handles, corners, strap contact — and a polished patch is worse than uniform semi-gloss because it changes size as the product turns.
How is material rustle measured reproducibly?
A calibrated sound level meter at 1 m with A-weighting, in a room under 30 dB(A) background, with a standardised pick-up, rotate, set-down and zip cycle at 0.5 m per second.
What sets the upper bound on mesh aperture?
Claw resistance. A monofilament above roughly 2.5 mm aperture is caught and pulled more easily, so larger apertures need a filament above 300 N tensile and a snag test.
Why does a textured shell help with LED flicker?
An LED panel with pulse-width dimming below about 1,500 Hz produces banding, and a smooth uniform surface makes the banding easy to see. A textured face breaks it up.
What is the most useful mounting provision for video?
A quarter-inch threaded insert in the base board, at 0.55-1.30 USD. It converts a product that has to be propped into one that mounts and removes the improvised clamps that damage shells.
What pull force should a magnetic closure have?
25-45 N, so that replacing a hook-and-loop closure for audio reasons does not compromise escape resistance.
What is in a camera test shot list?
A 360-degree pan, a 10-second static hold under a single key light, a zipper cycle at 1 m from a microphone, an interior shot through the mesh, and a pick-up and set-down cycle.
How much do four sample rounds cost?
165-430 USD for one colourway and 300-780 USD for three, credited against bulk orders above 1,500 units.
How much does video readiness add to unit cost?
3.05-8.00 USD on a 15.40 USD baseline, a 20-52% uplift. Taken selectively by shooting style it is 18% for a tripod review and 44% for a full rig package.
What does excess stock cost compared with air freight?
1,100 excess units at 17 USD carried for 12 months costs 2,200-3,700 USD in capital and warehousing, comparable to the air freight it was meant to avoid. Order to the midpoint when the forecast range exceeds 2.5 times.
Talk to QUANZHOU JUNYUAN BAGS about a pet carrier program: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample